Puzzled by a quote that came back higher than expected? The main cnc machining cost factors are machining time, material, tolerances, setups, finishing and order quantity. Change what you can in the design before quoting.
This page is part of the wider topic of precision cnc machining, which covers the process and its uses.
| Item | Value |
|---|---|
| Default tolerance when a drawing states none | ± 0.125 mm or better |
| Suggested wall thickness, metal parts | thicker than 0.8 mm |
| Suggested wall thickness, plastic parts | above 1.5 mm |
| Internal corner radius | at least one third of cavity depth |
| Hole depth to keep machining cost down | four times the diameter |
| Starting blank for a 500 g finished part | 2 kg or larger |
The first five figures come from a design-for-cost guide and the blank size from an engineering cost-reduction guide. Figures can change between suppliers and over time, so check the source before you rely on them.
Why do machining time and part complexity matter most?
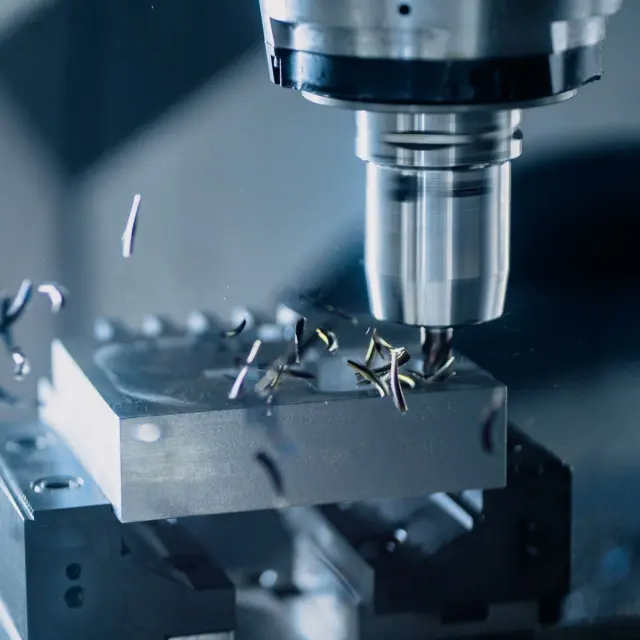
Machining time is often the main cost driver in CNC, according to a guide on design for machinability. The longer a part sits on the machine, the more you pay.
Complexity feeds straight into that time. Fictiv’s cost article notes that machining cost is directly proportional to design complexity, and that you also pay for setup time, the number of setups, programming time and machining time.
The gap can be large. In one example from a Chinese casting and machining supplier’s guide, a simple rectangular block with drilled holes might take 15 minutes, while a part with curves, bevels and tight radii could take 2 hours on the same machine.
An engineering cost guide lists features that commonly lengthen cycle time:
- Deep, narrow pockets: long tools, slow cutting, vibration and poor chip evacuation.
- Small internal radii: smaller cutters, lower rigidity, slower feeds and shorter tool life.
- Many hole sizes and threads: more tools, tool changes, setup checks and inspection.
- Complex surfaces: longer programming and finishing toolpaths.
Cutting tools typically work best in cavities up to two to three times their diameter, according to the same design guide. Going deeper tends to need special tooling or multi-axis machines.
Material and stock: what you pay for before cutting
Material affects the price twice: once when you buy the stock and again when you cut it. One manufacturing guide says soft metals such as aluminum cut quickly and generate less tool wear, driving down overall cost.
The same guide says hard metals such as stainless steel, titanium and Inconel require slower feeds, specialized cutters and more frequent tool changes, which significantly raise the price.
The per-kilogram price is only part of it. This supplier guide points out that what matters is how the material affects tool wear, machining time and scrap rate, and it notes that brass is expensive but machines easily, often reducing cycle time.
Stock size matters too. A finished part weighing 500 g may require a 2 kg or larger starting blank, and the engineering guide stresses that finished-part weight is not the same as purchased material weight.
How do tolerances and surface finish add cost?
Tight tolerances slow machining down, call for specialised inspection equipment and raise rejection rates, as the supplier guide explains. It describes a ±0.01 mm part as exponentially more difficult and expensive to produce than one at ±0.1 mm.
One automotive-industry article says dropping from plus or minus 0.005 to plus or minus 0.001 inches can double inspection time alone, according to Automotive Addicts. If a limit does not affect how the part works, question whether it needs to be there.
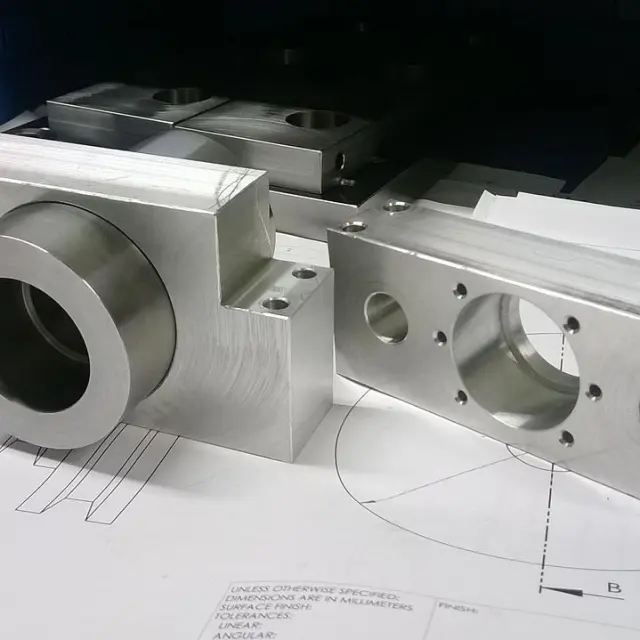
When a drawing states no tolerance, parts are machined to a standard of ± 0.125 mm or better, which the design guide calls sufficient for most non-critical features. For more on how limits are specified, see these notes on cnc machining tolerances.
Surface requirements work the same way. The engineering guide lists unnecessary finishes as a cost escalator because of subcontracting, masking, inspection and minimum-order charges, and suggests limiting premium finishing to functional areas such as:
- Mating and locating surfaces
- Sealing surfaces
- Bearing and sliding surfaces
- Cosmetic faces
Our overview of cnc surface finishes shows which options exist before you decide what each face needs.
Setups, tooling and order quantity
Every extra setup adds operator time, coordinate re-establishment, clamping verification, alignment risk and potential scrap, according to the engineering guide. It adds that a geometrically simple part requiring six orientations may cost more than a more complex part machined in one or two setups.
Machine type plays a part as well. Automotive Addicts says multi-axis and advanced work costs more because of longer cycles and harder programming.
Quantity changes the unit price because programming and planning are largely fixed. A single prototype and a batch of 100 parts both require core programming, process planning and any custom tooling or gauges, which is why one-off parts usually have a higher unit cost.
The supplier guide adds that frequent small runs with design changes may incur repeated setup costs, so batching repeat orders can lower the total.
Finishing, inspection and market factors
Work done after cutting is easy to overlook. The engineering guide names these finishing steps as part of the cost:
- Anodizing, bead blasting, plating, passivation and painting
- Heat treatment, grinding and polishing
- External transport and queue time
- Masking, secondary inspection and rework risk
Outside factors move the price as well. The manufacturing guide says labor costs vary by region and that material prices fluctuate, particularly for steel, aluminum and titanium.
Imported or specialty materials can add sourcing costs, customs duties and minimum order quantities, a point made in the supplier guide. It also says pricing usually falls into per-part pricing or hourly machine rates, so check which one your quote uses.
Design choices that lower the price
The engineering guide frames cost reduction as removing unnecessary material, machine time, setups, tooling, inspection and finishing, not squeezing supplier margin. Fictiv also advises following all Design for Manufacturability feedback.
These design rules come from the design-for-cost guide:
- Add an internal radius of at least one third of the cavity depth, and use the same radius throughout to avoid tool changes.
- Limit thread length to three times the hole diameter at most.
- Use standard hole sizes, because non-standard sizes need an extra machining step.
- Limit hole depth to four times the diameter.
- Define tighter tolerances only where they are absolutely necessary.
Do not go too far, though. The engineering guide cautions that less material is not always cheaper, because walls that are too thin can deform, vibrate or scrap during machining.
Frequently asked questions
Why is a single prototype so expensive per part?
Show answer
Programming, process planning and any custom tooling are needed whether you order one part or 100. With one part, those fixed costs fall on that single unit, as the engineering guide explains.
Do tighter tolerances always cost more?
Show answer
Generally yes, because they mean slower machining, more inspection and higher rejection risk, according to the supplier guide. Specify them only where the part’s function needs them.
Is aluminum always the cheapest material?
Show answer
Not necessarily. Aluminum is easy to cut, but the supplier guide at china-casting.com notes that tool wear, machining time and scrap rate all matter, and that brass, though expensive, can cut cycle time.
Does removing material always lower the cost?
Show answer
No. Thin walls can deform or vibrate and end up as scrap. The design guide suggests metal walls thicker than 0.8 mm and plastic walls above 1.5 mm.